沧州铭添管道有限公司
诚信经营
价格合理
可按需求定制
全国咨询热线
182-3276-4999
欢迎来到沧州铭添管道有限公司!
×182-3276-4999

通过微信扫一扫
获取螺旋管今天价格
客户服务热线
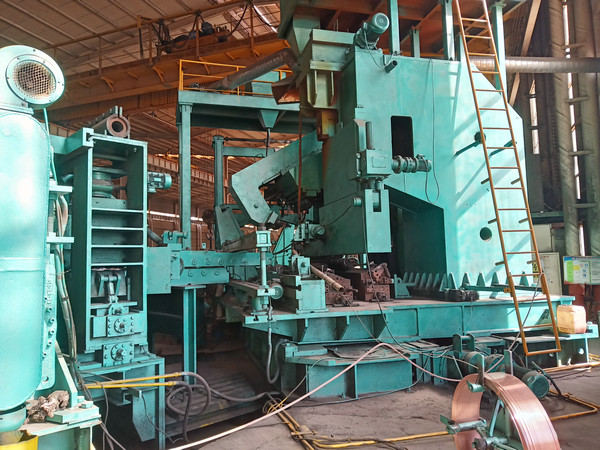
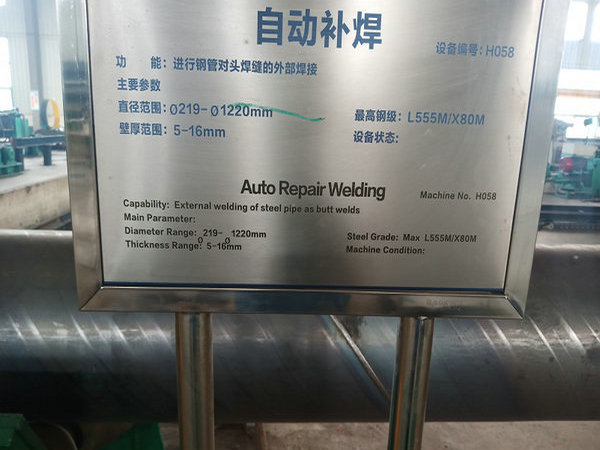
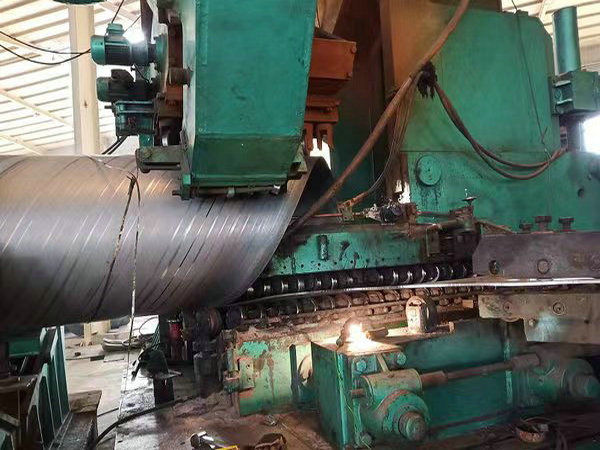
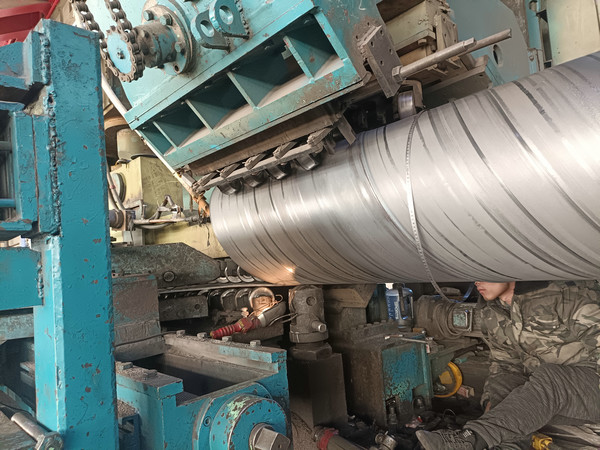
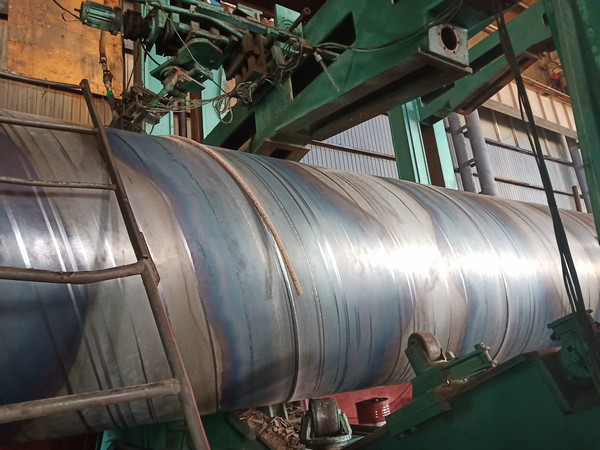
182-3276-4999AWWA C200-2023标准钢制水管焊接资格要求:1、概述:自动或手动焊接操作员和焊接程序应符合ASME锅炉和压力容器规范第九节、AWS B2.1或AWS D1.1/D.1.1M或买方和制造商共同商定的任何其他规范的要求。表1中列出的材料应符合ASME BPVC第九节P-No.1、第1组、第2组或第3组材料分组的要求。当第4.5.2节中对母材的评估确定需要夏比试验时,适用的焊接工艺应具有缺口韧性,以满足与母材相同的要求。2、自动焊接:在可行的情况下,直管段和特殊管段的螺旋焊缝、线圈拼接焊缝、纵向焊缝和环焊缝应使用自动焊机焊接。根据要求,应将焊缝样品提交给买方进行测试。3、手工焊接:当使用自动焊机不切实际时,应允许手动焊接环缝和特殊部分,并完成线圈拼接焊缝。在直管段上,在连续制管过程中,手工焊接仅允许用于线圈和板材的定位焊,以进行焊接。4、在管道内部,重新焊接和修复板材和自动机器焊缝中的结构不连续性,以及本标准中允许的其他情况(第4.7节)。根据要求,应将焊缝样品提交给买方进行测试。5、端部焊接:熔焊管纵向焊缝的端部焊接,如果不是通过自动埋弧焊或自动保护电弧焊完成的,则应由符合第4.6.1节规定的合格操作员完成。
AWWA C200-2023 Standard Steel Water Pipe Welding Qualification Requirements: 1. Overview: Automatic or manual welding operators and welding procedures shall comply with the requirements of ASME Boiler and Pressure Vessel Code Section IX, AWS B2.1 or AWS D1.1/D1.1M, or any other specification mutually agreed upon by the buyer and manufacturer. The materials listed in Table 1 shall comply with the requirements of ASME BPVC Section IX P-No.1, Group 1, Group 2, or Group 3 material grouping. When the evaluation of the base metal in section 4.5.2 determines the need for Charpy testing, the applicable welding process should have notch toughness to meet the same requirements as the base metal. 2. Automatic welding: Where feasible, spiral welds, coil splicing welds, longitudinal welds, and circumferential welds on straight and special pipe sections should be welded using automatic welding machines. According to the requirements, weld samples should be submitted to the buyer for testing. 3. Manual welding: When using an automatic welding machine is impractical, manual welding of circumferential seams and special parts should be allowed, and coil splicing welds should be completed. On the straight pipe section, manual welding is only allowed for positioning welding of coils and plates during the continuous pipe making process for welding. 4. Within the pipeline, re weld and repair structural discontinuities in the plates and automatic machine welds, as well as other situations allowed in this standard (Section 4.7). According to the requirements, weld samples should be submitted to the buyer for testing. 5. End welding: The end welding of longitudinal welds in fusion welded pipes, if not completed by automatic submerged arc welding or automatic shielded arc welding, shall be carried out by qualified operators in accordance with Section 4.6.1.
本文版权归 沧州铭添管道有限公司 所有;本文共被查阅 1012 次。
当前页面链接:http://wapipe1.com/industry/2539.html
未经授权,禁止任何站点镜像、采集、或复制本站内容,违者通过法律途径维权到底!
期待与您的合作,欢迎给我们留言或直接拨打:182-3276-4999
留下您的信息,我们将第一时间和您取的联系!
版权所有:沧州铭添管道有限公司 Sitemap
24小时/热线:182-3276-4999 冀ICP备2021012226号-5
扫码添加微信好友